Hey there, I’m Jake, and if you’ve ever worked with process piping, oil and gas, water treatment, or any industry that relies on tight shutoff valves, you know ball valves are workhorses. But here’s the thing – even the best ball valves on the market won’t do their job if they leak. Not just the small, annoying kind that drips onto the floor, but the critical kind that can throw off whole operations, waste resources, or even create safety risks. That’s why, as a ball valve supplier, I get asked all the time: “How do you actually measure a ball valve’s leakage rate? Not just the basic ‘does it hold pressure’ test, but the real, reliable number that tells us if this valve is going to perform when we need it to.” Ball Valves
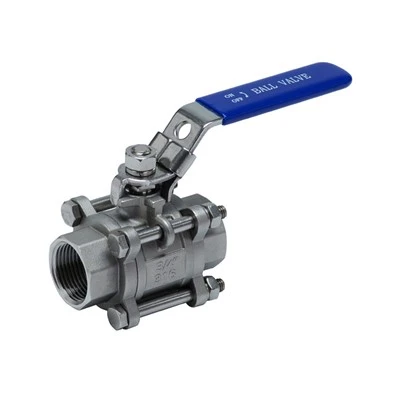
I’ve been in this game for 12 years, so I’ve seen the good, the bad, and the straight-up wrong ways people test leakage. A lot of shops cut corners to get a quick pass, but that’s a gamble. Today, I’m breaking down how we do it at our facility, why the steps matter, and what you should look for so you don’t end up with a valve that looks great on paper but fails when it counts.
First, let’s get one thing straight – leakage rate isn’t a one-size-fits-all number. It depends on what standard you’re working to, right? Most industries reference either API 6D (for pipeline valves), ASME B16.104 (for industrial valves), or ISO 5208. Those standards outline exactly how to test, what pressure to use, and how to calculate leakage. I always tell clients, “If your test isn’t aligned with the standard your project requires, the number you get is useless.” Don’t let anyone sell you a valve that’s tested to a lower spec than what your job needs.
Now, let’s walk through the actual process, step by step, like I’m showing it to you in our test lab.
Step 1: Prep the Valve (No Shortcuts Here)
Before we even connect a gauge, the valve has to be spotless. Old gaskets, metal shavings, dirt, or even leftover paint inside the body will skew results – even a tiny piece of debris can sit between the ball and seat and create a false leak. We take every valve we test, disassemble it completely, blast the body and ball with media (usually glass beads or walnut shells, depending on the material), and then run it through a compressed air blowdown. We also check the seats themselves for scratches or manufacturing defects. If there’s a tiny nick in a PTFE seat, that’s going to leak – no amount of testing will fix that.
Then, we lubricate the seats properly. Wait, not too much, not too little. Over-lubricating can leave a film that looks like a leak when you pressurize, and under-lubricating means the ball doesn’t seat evenly. We use the same lubricant that the valve will see in service too – if it’s a valve for a chemical plant, we use a chemical-resistant lubricant, not generic grease. That way, we’re testing real-world performance, not a lab-controlled scenario.
Step 2: Set Up the Test Rig (Calibrate First, Always)
Next, we mount the valve to our test skid. The rig has two pressure ports: one for upstream pressure (that’s the side we pressurize, simulating the line pressure the valve will handle) and one for downstream (the side we measure leakage on). We also have a precision pressure transducer – not a cheap analog gauge that’s off by 5%. We calibrate that transducer every 30 days, traceable to national standards, so we know our pressure readings are dead-on.
One big thing people mess up here: if it’s a flanged valve, we use the correct gaskets and torque the bolts to the exact spec. If you under-torque, the pipe joint leaks, not the valve. Over-torque, and you warp the valve body, which can mess up the ball seating. We use a torque wrench every time, no exceptions.
Step 3: Choose the Test Medium (Gas vs. Liquid – Big Difference)
Here’s where a lot of first-timers go wrong: picking the wrong test medium. Leakage rates are different for gas vs. liquid, and the standard will tell you which to use. For example, API 6D allows gas or liquid, but gas testing is more sensitive because it’s compressible – even a tiny leak will show up as a pressure drop, whereas liquid might hold pressure longer because it’s incompressible. But wait, gas is more dangerous, right? So we never test with compressed air above the rated pressure without safety guards. We use nitrogen for high-pressure gas tests – it’s inert, so no risk of ignition if something goes wrong.
For liquid tests, we use water, usually at ambient temperature, unless the valve is rated for extreme temps – then we’ll use the actual process fluid (or a simulant) to get accurate results. Just last month, we tested a valve for a food and beverage client, so we used deionized water to avoid contaminating the test – that’s the kind of detail that makes a reliable test, not just a box-ticking exercise.
Step 4: Pressurize and Stabilize (Wait, Don’t Rush This)
Okay, we mount the valve, connect the transducers, close the downstream valve, then slowly pressurize the upstream side to the test pressure. Not all the way at once – we ramp it up to 50% of the test pressure first, hold for 5 minutes, check for any obvious leaks, then go up to full test pressure. The stabilization part is key here. The valve will expand a tiny amount when pressurized, the pipe will expand too, and air bubbles can escape from the test medium (if using liquid). We hold for 10 to 30 minutes, depending on the standard, before we start measuring leakage. If you start counting leaks too early, you’ll get a number that’s way higher than actual – that’s a false positive, and it’s unfair to the valve.
Step 5: Measure Leakage (Two Common Methods – Know Which One Your Test Uses)
Now the fun part: actually measuring how much is leaking past the ball. There are two main methods, and the standard will specify which to use.
First, the Pressure Drop Method. This is the most common for gas tests. Once stabilized, we close the upstream isolation valve (wait, no – actually, most standards say you leave the upstream pressure regulated, but some use a closed upstream side to measure pressure decay over time). Wait, let me clarify: for the pressure decay method, after stabilizing at test pressure, we isolate the upstream side, then monitor the downstream pressure (or the upstream pressure, depending on setup) for a set time. The leakage rate is calculated from the change in pressure, temperature (we also monitor temp, because pressure changes if temp shifts), and the volume of the downstream chamber. For example, if the downstream volume is 1 liter, and pressure drops 0.1 psi in 10 minutes at 70°F, we can calculate how many standard cubic centimeters per minute (sccm) is leaking past. That’s the unit you’ll see for gas leakage – sccm, or sometimes bubbles per minute (but sccm is more accurate).
The second method is the Bubble Count Method, which is super common for low-pressure gas tests. We have a graduated container filled with water, with a tube leading to the downstream side of the valve. Any gas leaking through the valve will bubble through the water, and we count how many bubbles come out in a minute. We do this for 5 minutes, take an average, and that gives us the leakage rate. It’s simple, but it works great for small leaks – we can catch a leak that’s too small to show up on a pressure drop gauge.
For liquid tests, we use the Liquid Level Method. The downstream side is connected to a graduated cylinder, and we measure how much liquid collects over a set time. That’s usually in milliliters per minute (mL/min) or drops per minute, depending on the size. I’ll be honest – liquid tests are less sensitive, because liquid doesn’t compress, so a tiny leak might not show up as a pressure change, but it will show up as liquid in the cylinder.
Step 6: Compare to the Rated Leakage Class (This Is What Actually Matters)
Once we have our number, we compare it to the leakage class the valve is rated for. Let’s talk about the most common classes, because this is where most people get confused. For ball valves, the standard classes are A through F, with A being the most leakage (for isolation only, not tight shutoff) and F being zero-leak (for critical applications). Wait, let’s get the numbers straight:
- Class A: Up to 10,000 sccm (gas) or 100 mL/min (liquid) – basically for on/off, no tight shutoff needed.
- Class B: 100 sccm gas, 10 mL/min liquid
- Class C: 1 sccm gas, 0.1 mL/min liquid
- Class D: 0.1 sccm gas, 0.01 mL/min liquid
- Class E: 0.01 sccm gas, 0.001 mL/min liquid
- Class F: No measurable leakage (we can’t detect it with our equipment)
So if a client needs a valve for a gas pipeline that’s transporting natural gas, they’ll need Class E or F, not Class B. I’ve seen clients get burned because they ordered Class B valves and thought they were Class C – the difference is night and day.
Now, let’s bust a common myth here: a lot of people think “zero leakage” is possible, but really, Class F is just below the detection limit of the test equipment. Even the best ball valves will have an atom-sized leak, but it’s so small you can’t measure it, so it doesn’t matter for 99% of applications.
But wait, there’s also seat leakage vs. body leakage. We always check both! The leakage rate we measure is total leakage, but we also test body leakage separately by blocking the seats and pressurizing the body. If the body leaks, that’s a manufacturing defect – a casting flaw or a bad weld. Body leakage is way worse than seat leakage, because it means the valve itself is broken, not just the shutoff.
Now, what about common mistakes we see clients make when testing? I can tell you from experience: a lot of guys will test the valve at ambient pressure, not the actual working pressure. Or they’ll use air for a valve rated for water, which gives a different leakage number. Or they’ll rush the stabilization time, so they get a wrong number. And some people use a bucket of soapy water on the valve’s connections to look for bubbles – that’s fine for a quick check, but it’s not an accurate measurement. Soapy bubbles will show you if there’s a leak, but they won’t tell you how much, which is what you need for compliance.
As a supplier, we don’t just send you a valve with a test sticker that says “passed.” We send you a full test report, with the test medium, pressure, stabilization time, leakage number, and which class it meets. If you need a specific test method, like per API 6D or ISO 5208, we’ll adjust our process to match exactly. We even do high-temperature tests for valves that will see 500°F, and cryogenic tests for valves for LNG, because leakage changes with temperature too – the seats get harder or softer, so the leakage rate isn’t the same at room temp as it is at -200°F.
Here’s the thing: measuring ball valve leakage rate isn’t rocket science, but it’s not something you want to leave to chance. If you cut corners on testing, you could end up with a valve that leaks so much you’re wasting product, or worse, causing a safety hazard. I’ve had clients come to us after buying cheap valves from another supplier, only to find out their leakage rate was 10x higher than rated, and they had to replace half their valves 6 months after installation. That’s a cost no one wants to deal with – not to mention the downtime.
If you’re working on a project right now and you need ball valves, or you’re confused about what leakage class you actually need, I’m here to help. We can work with your engineering team to figure out the right testing spec, provide you with test reports every step of the way, and make sure the valves you get are exactly what you need, no surprises. Just reach out to our team, and we’ll walk you through every detail – no sales jargon, no hidden fees, just honest advice from a guy who’s been in this business long enough to know what works.
Castings References
API Standard 6D, Pipeline Valves, 24th Edition, American Petroleum Institute, Washington, D.C., 2020.
ASME B16.104, Industrial Valves – Seat Leakage Test Methods, American Society of Mechanical Engineers, New York, N.Y., 2018.
ISO 5208, Industrial Valves – Pressure Testing of Valves, International Organization for Standardization, Geneva, 2015.
United Brothers Metal Products Co., Ltd.
United Brothers Metal Products Co., Ltd. is one of the most professional ball valves manufacturers and suppliers in Vietnam. We are committed to providing high quality customized products with competitive price. Please feel free to buy bulk durable ball valves in stock here from our factory. Also, pricelist is available.
Address: Lot 61c2, 99a Long Giang Industrial Park, Tan Phuoc 3 Commune, Dong Thap Province, Vietnam
E-mail: sales@ubfittings.com
WebSite: https://www.ubvalves.com/
